Before01
Company overview
- Counting done by eye
- Errors from stacking
- Missing count records
AI
Zero-defect quality management completed by precise, vision-AI-based inspection
OVERVIEW
From image capture through pre-processing and feature extraction to judgment and feedback, as one flow.
Cameras and lighting photograph each part under the same conditions every time.
Noise removal and normalization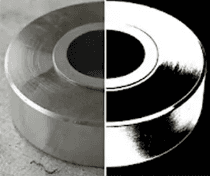
Noise is removed and brightness and size are normalized, so the image is ready for analysis.
AI pattern analysis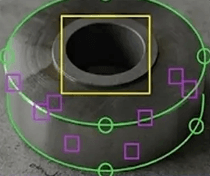
A trained AI model finds the features a judgment needs, such as shape and defect location.
Pass/fail judgment
Each part is judged good or defective, and the result is fed back into process improvement.
Feedback to image captureKEY FEATURES
From surface inspection through defect detection and dimensional measurement to quality statistics.
Vision Capability
01 / 04
01
It instantly detects minute defects with a high-performance vision system and deep-learning algorithms. By establishing a uniform quality standard with no variation between operators, it raises shipment reliability.
Management Scope
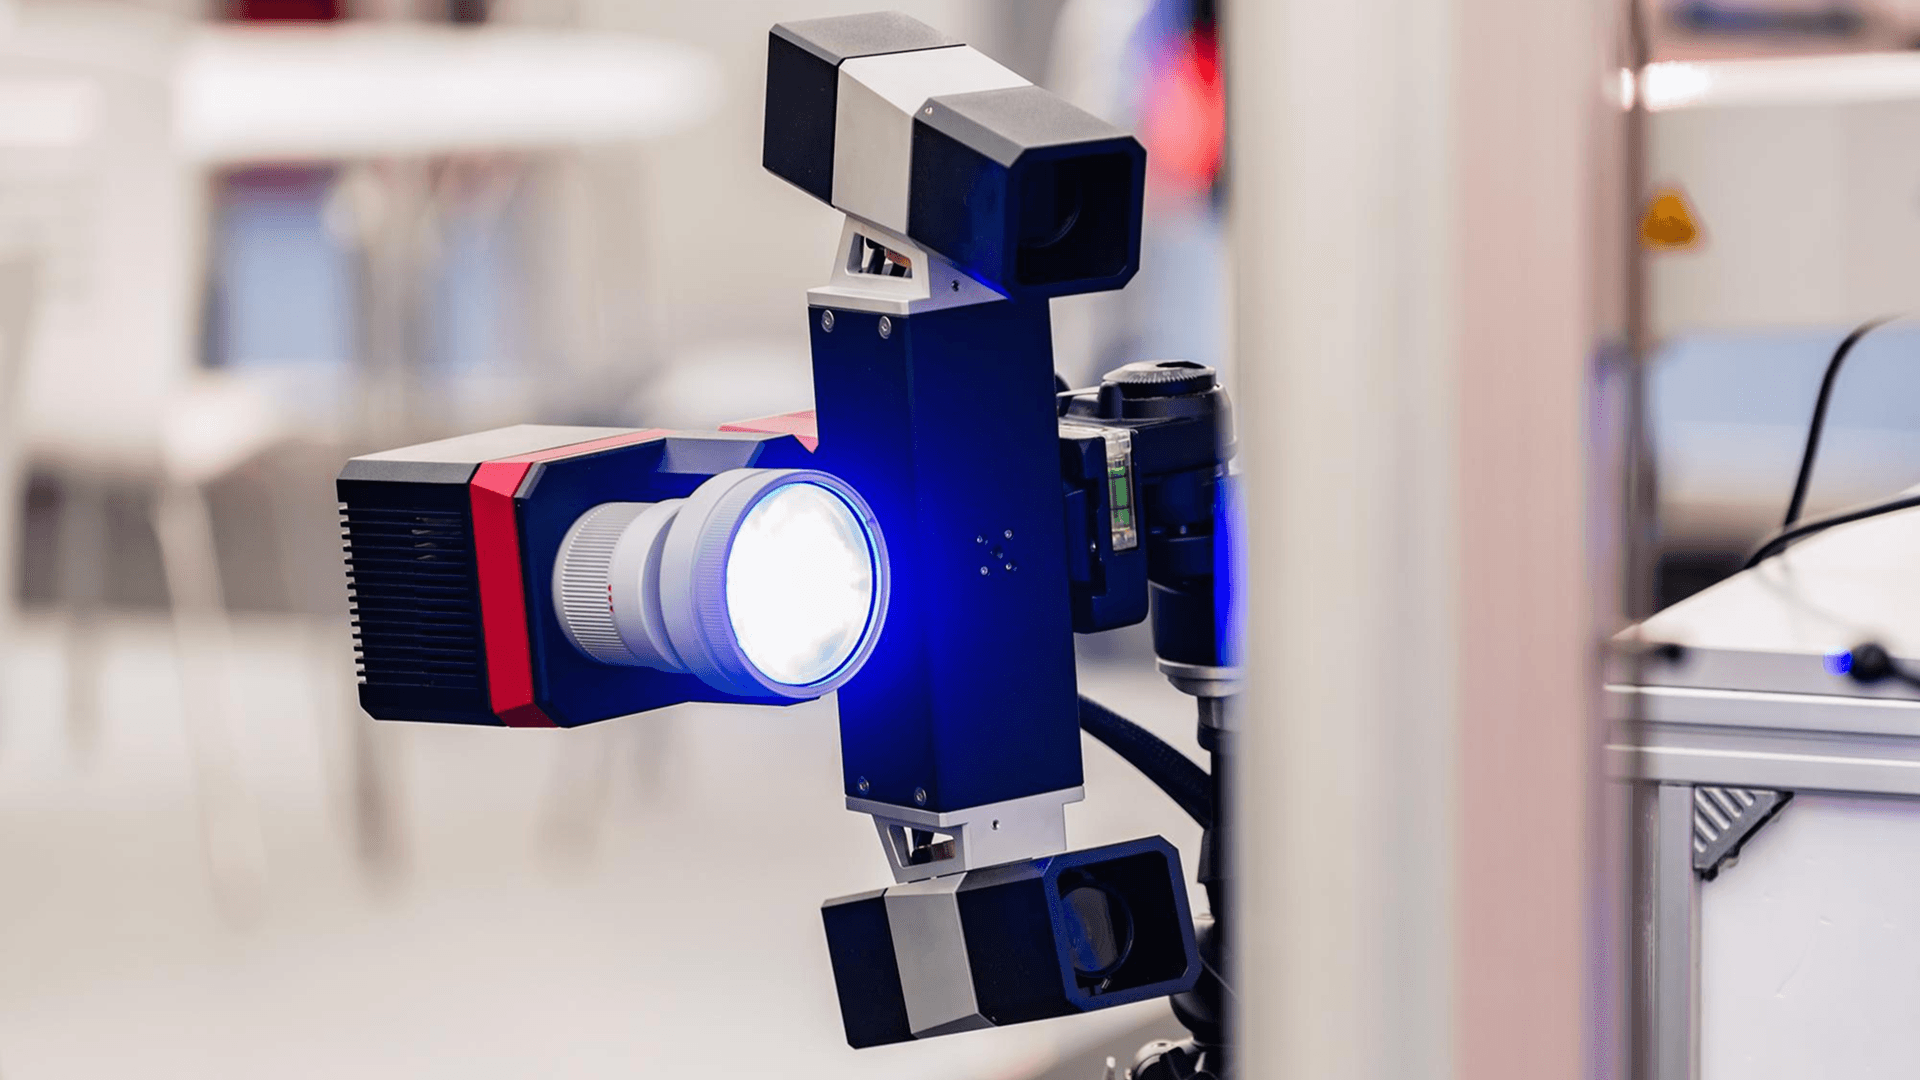
Real-time image capture
High-resolution cameras and optics capture surface images during production in real time
WORKFLOW
For each capability, the order it runs in and the check it passes before moving on.
Capture design
camera · lighting · distance
Timing linkage
speed · sensor trigger
Image correction
brightness · resolution · region
Quality check
blur · occlusion · exposure
Recorded alongside
Capture position/
Trigger/
Raw/
Is the inspection target clearly visible?
Valid image → model judgment
Occluded/blurred → recapture · review
An example workflow · the detailed links and criteria are set to suit your floor.
SYSTEM ARCHITECTURE
From the data that goes in to the results on the floor.
01 / INPUT
CONNECTED OPERATIONS
AI Vision
03 / OUTPUT
01 / INPUT
CONNECTED OPERATIONS
AI Vision
CONNECTED OPERATIONS
AI Vision
03 / OUTPUT
METHOD
Floor imagery gathered and learned, then returned as a verdict.
Data Ingestion
Line-scan camera
3D vision sensor
Thermal camera
Lighting correction · resolution normalization
Tied to conveyor speed · precise capture timing
Target System
AI/ML Modeling
Analysis & prediction
Object detection
YOLO v10, 11
Defect segmentation
Scratches · pinholes · cracks
Defect classification
CNN, Transformer
3D measurement
Shape deviation · dimensions
Feedback & refinement
Operational visibility
Process root cause
Failure prediction
Instant alerts past thresholds / automatic equipment stop
Electronic components
Robot vision
Automotive
Precision machining
Secondary batteries
Food/pharmaceuticals
Electronic components
Robot vision
Automotive
Precision machining
Secondary batteries
Food/pharmaceuticals
A camera judges every piece, including the flaws a person misses.
EFFECT
What it leaves behind — in detection rate, misses, false rejects and inspection effort.
Higher detection rate
High-resolution imaging and deep learning catch the fine defects the eye misses, and hold one standard with no drift between judgments.
Fewer misses
Every unit is inspected, so nothing slips through a sample, and a model per defect type learns the patterns that are easiest to miss.
Fewer false rejects
The boundary that used to call a good part bad is re-set from data, so sound product stops being scrapped or re-run.
Less inspection effort
Inspection staff move to higher-value work, and the time spent re-setting the line for a different item comes down.
CASE STUDY
Manual counting automated, taking accuracy to around 99.9%.

Customer industry
Primary steel manufacturing
Before01
After02
Business impact
Inspection automation where AI vision does the counting

